The Guideway Selection Debate in Modern Machine Tools #
Machine tool guideways perform two critical functions: guiding the moving carriage along a precise geometric line and supporting the massive cutting forces generated between the cutting tool and workpiece.
Historically, the industry debated between friction-based Box Ways (Hardened Cast Iron Sliding Ways) and low-friction Linear Guideways. However, the advent of Heavy-Duty Roller Linear Guideways has fundamentally redefined the modern balance of speed, rigidity, and longevity.
1. Structural Comparison: Contact Area vs Coefficient of Friction #
- Box Ways (Sliding Contact): Utilize a large surface-to-surface cast iron contact area lubricated by an oil film and Turcite-B anti-friction lining. They offer unmatched vibration dampening during heavy interrupted roughing on forged steel or high-nickel alloys. However, their friction coefficient is relatively high (0.05 - 0.1), limiting rapid traverse speeds to 12–16 m/min and introducing stick-slip during micro-feeding.
- Ball Linear Guides: Feature point-contact recirculating steel balls. Extremely fast (up to 48 m/min), but susceptible to elastic deformation under heavy cutting loads.
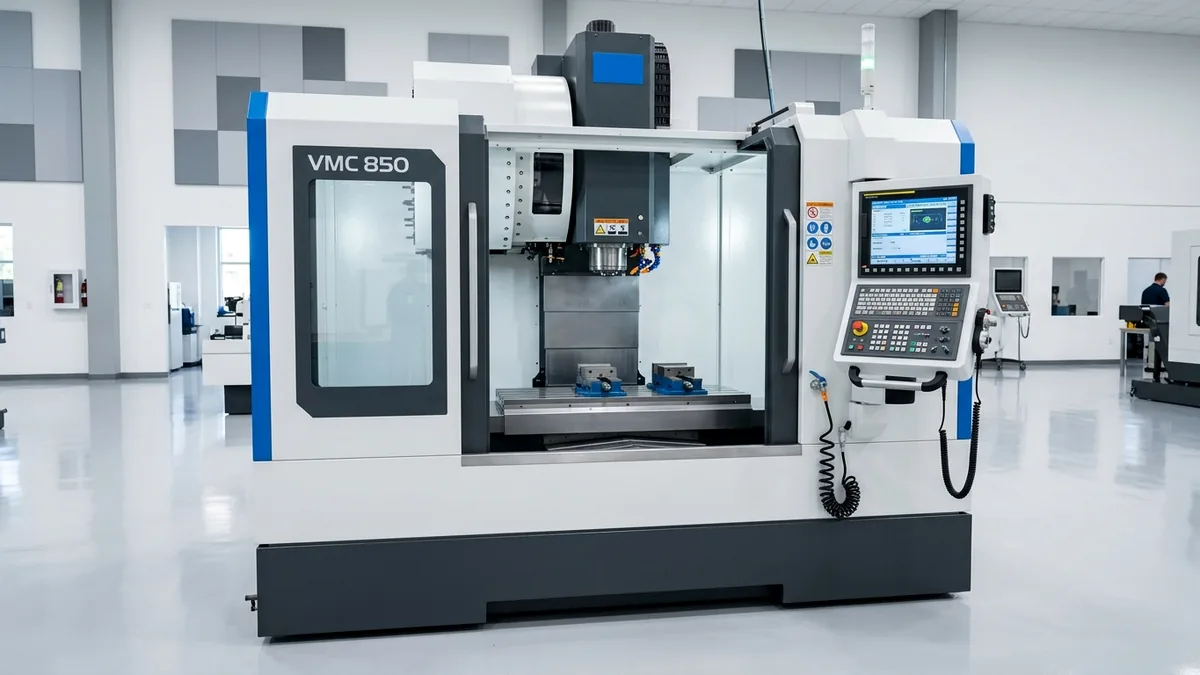
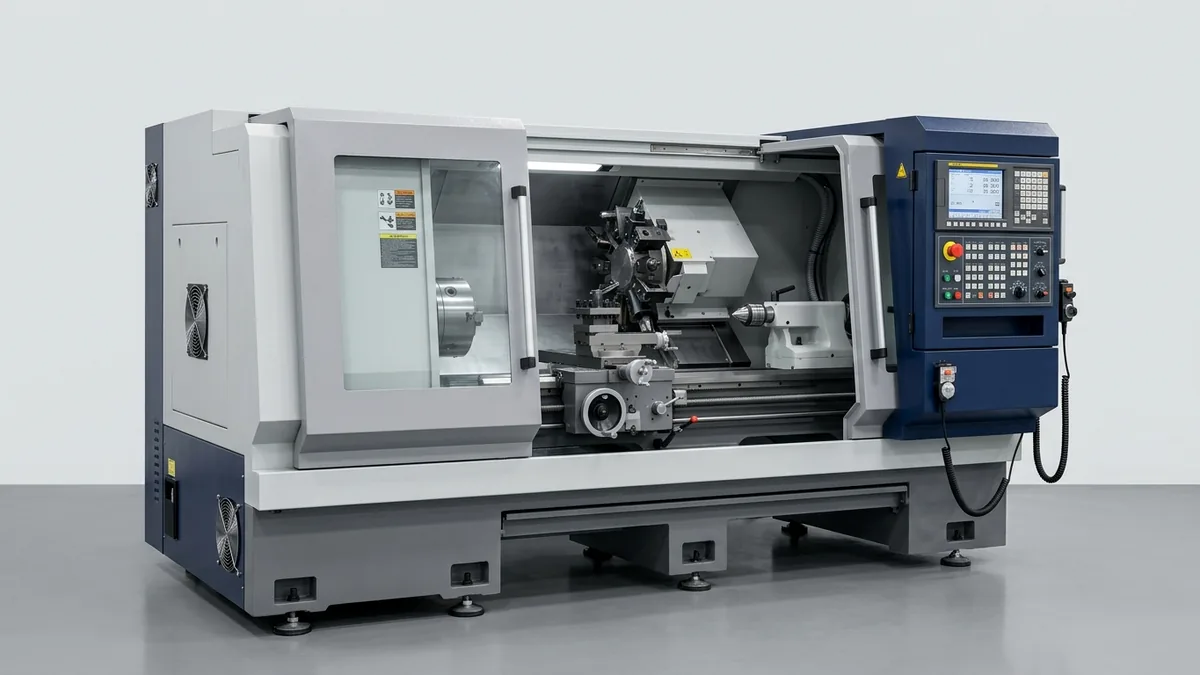
- Roller Linear Guides (DAHAN Standard on VMC850/855 & TCK Series): Replace point-contact balls with cylindrical precision rollers. Cylindrical rollers provide line contact, delivering up to 90% of the rigidity of box ways while maintaining the near-zero friction and 36 m/min rapid speeds of linear guideways.
2. Dynamic Performance Matrix #
| Engineering Factor | Box Ways (e.g. CK Series Bed) | Roller Linear Guides (e.g. VMC Series) |
|---|---|---|
| Coefficient of Friction | 0.05 ~ 0.10 (Requires heavy oil) | 0.002 ~ 0.005 (Ultra-low resistance) |
| Rapid Traverse Rate | 8 ~ 16 m/min | 24 ~ 36 m/min |
| Stick-Slip at Micro-Feed | Possible under heavy static friction | Zero stick-slip, true sub-micron steps |
| Damping of Interrupted Cuts | Exceptional | Excellent (with roller pre-load) |
| Maintenance & Replacement | Requires hand-scraping & refitting | Precision modular rail replacement in hours |
3. Which System Fits Your Factory Production? #
- Choose Roller Linear Guides (DAHAN VMC850, VMC855, TCK50, TCK52):
- If your production involves complex 3D mold surfacing, high-speed aluminum cutting, rapid peck drilling, and high-volume batch parts where acceleration directly dictates your hourly profit.
- Choose Hardened Induction Box Ways (DAHAN CK6150, CK6160):
- If you routinely machine heavy raw forgings, cast iron housings with scale, large oilfield pipe couplings, or long industrial rollers with aggressive interrupted cuts.
Have specific material challenges? Consult DAHAN CNC application engineers at xiuc32860@gmail.com to optimize your machine configuration.